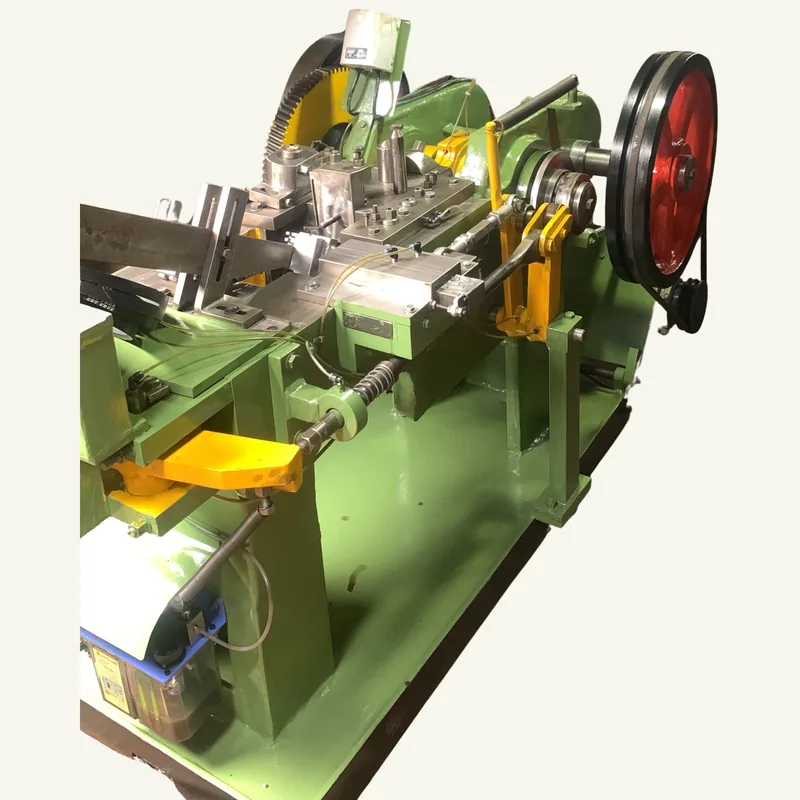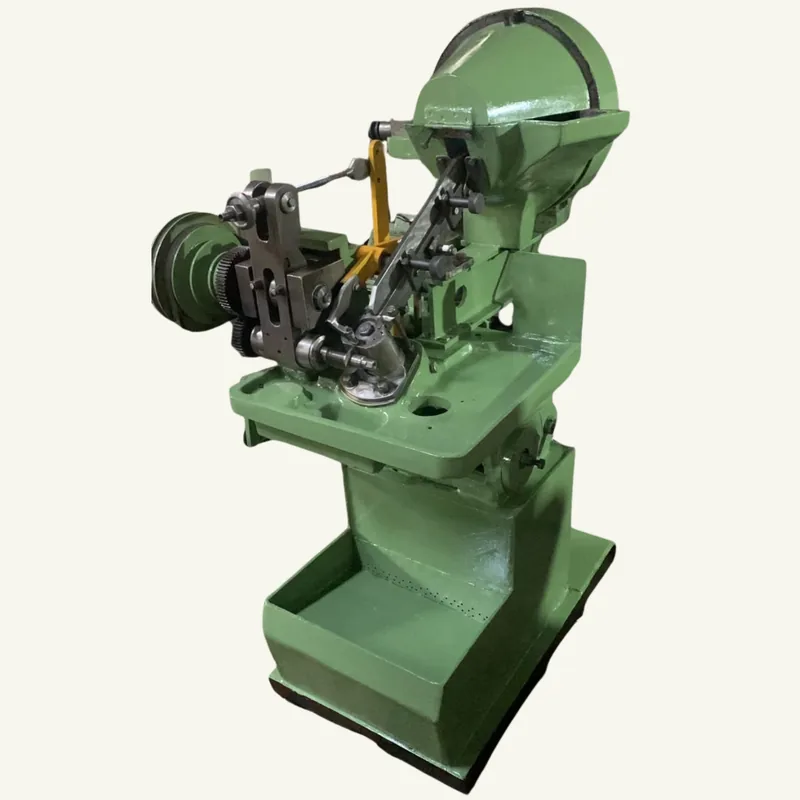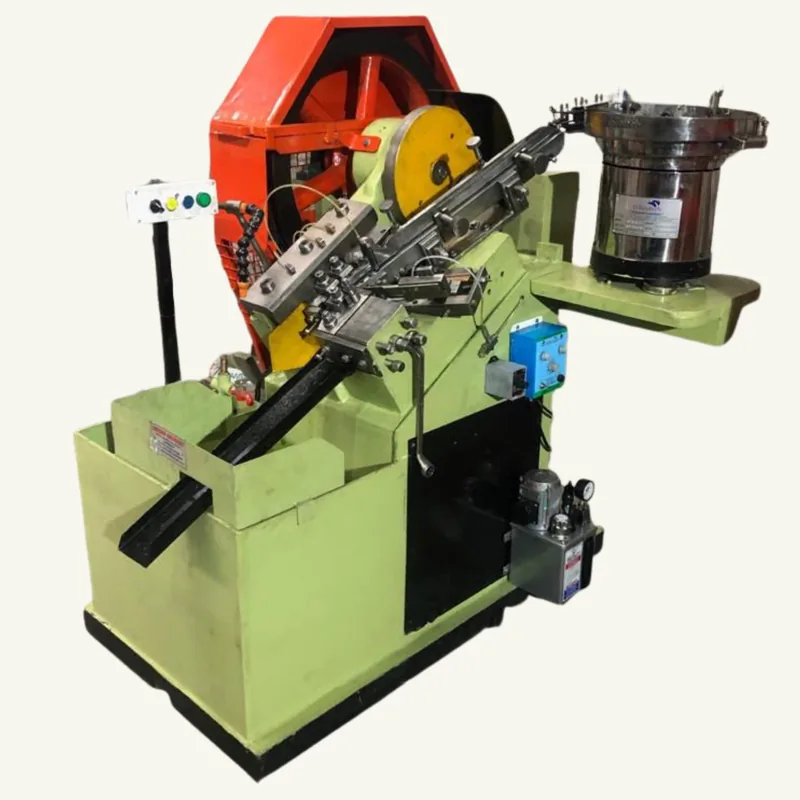
H series
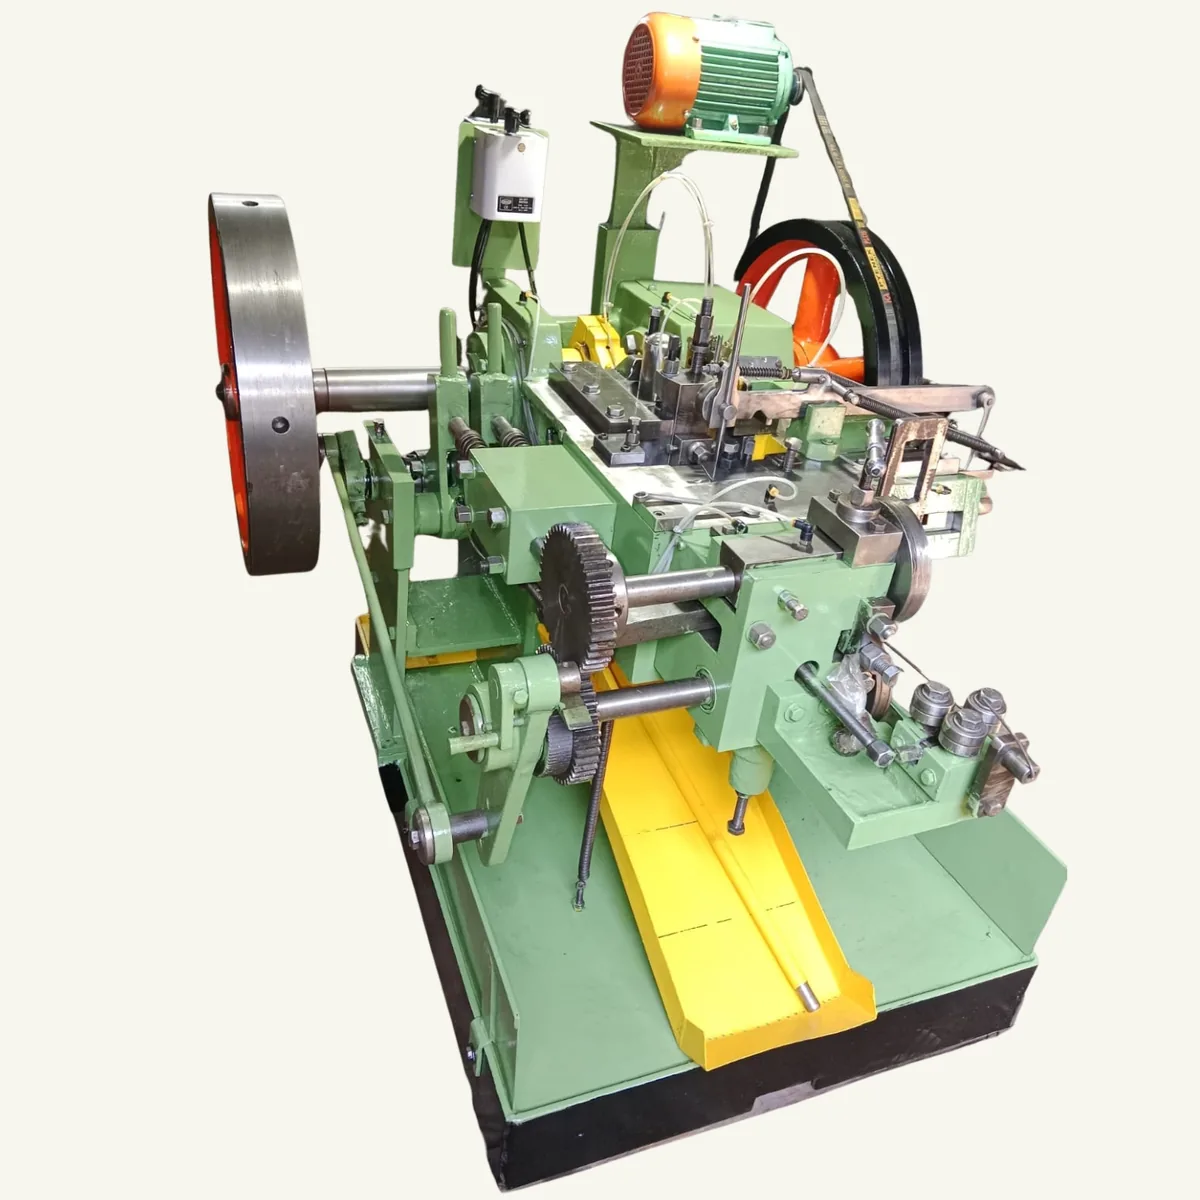
Wire goes in, a formed head comes out, up to 145 times a minute. Seven models cover wire from 0.8 to 10 mm, for screws, bolts, rivets and pins.
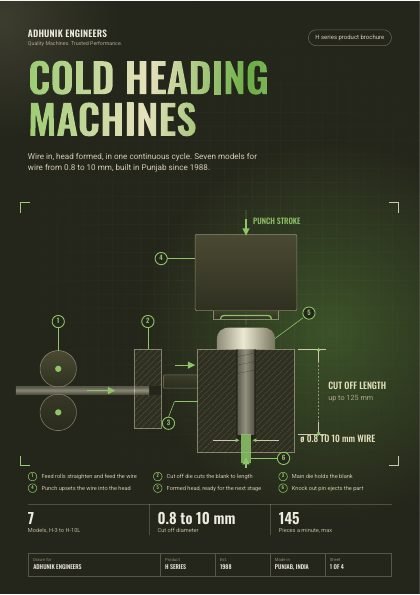
Scroll through a single cycle of the header. Each step lights up the part doing the work.
Feed rolls draw the wire off the coil and straighten it on the way in.
The cut off die shears a blank to exactly the length the head will need.
The transfer carries the blank across and into the main die.
The punch strikes and upsets the end of the wire into the head. Cold, with no heating and no metal cut away.
The knock out pin pushes the part out, and the next blank is already on its way.
Tap a model to see its numbers, its blank size and its tooling.
Blank drawn to the same scale for every model. Dashed outline is the H-10L.
 All seven models, side by sideEvery specification, die size and feature in the 4 page brochure.Download PDF
At full speed
Max output from the published specification. Real output depends on part length, head and material.
Die and punch sizes for the selected model, drawn to scale. Spares for every size are kept in stock.
Holds alignment under continuous heading loads. The frame is the reason a header still runs true after years of heading.
Shear before the machine is damaged if something jams.
Quieter ejection of each formed part, for a calmer shop floor.
Easy access and adjustment of the punch.
Quick setting when you change the job.
For long life in round the clock running.
For most M3 screws the H-3 is the starting point. For longer blanks, above about 23 mm under head, the H-4 has the extra cut off length.
Yes. Recessed heads are formed by the punch in the header, so no extra machine is needed for them.
How it works, features and every specification, in 4 printable pages.